Hawthorn extract, derived primarily from the leaves, flowers, or berries of Crataegus pinnatifida or Crataegus oxyacantha, is recognized worldwide as a foundational ingredient in cardiovascular support formulas. The efficacy of hawthorn is tied directly to its complex phytochemistry, most notably its concentration of oligomeric proanthocyanidins (OPCs), flavonoids (such as vitexin, vitexin-2"-O-rhamnoside, hyperoside, and rutin), and organic acids. Global health food and dietary supplement manufacturers require ingredients that offer not just biological activity, but rigorous consistency across batches.
As experienced suppliers of wholesale hawthorn extract, Botanical Cube Inc., together with Shaanxi Tianben Kangyuan Biotechnology and our parent company Xi'an Tianben Bioengineering Co., Ltd., implements scientific oversight at every step. From the cultivation and selection of raw botanicals to advanced chromatographic validation, we ensure that every batch matches the strict parameters demanded by modern health product developers.
In our interactions with hundreds of global procurers, we have identified key pain points in the botanical supply chain: batch-to-batch color drift, poor water solubility in beverage applications, pesticide residue, and varying active ingredient claims. Choosing a supplier that lacks proper chromatographic testing leads to formulation instability and regulatory risks.
We combat these issues directly. Botanical Cube Inc. provides transparent HPLC (High-Performance Liquid Chromatography) analysis for vitexin and UV-Vis spectrophotometry for total flavones. Standardizing these botanical fractions provides product developers with predictable performance in tablet compression, capsule filling, and hot/cold water dissolution systems.
Standardized vitexin levels and total flavones verified via HPLC, eliminating batch variability and securing formulation uniformity.
Rigorous control of heavy metals, pesticides, and PAHs to meet USP, European Pharmacopoeia, and China Food Standards.
Specialized physical processing options designed for instant hot-water and cold-water solubility in functional drinks.
The future of hawthorn extract lies in preserving fragile botanical compounds while keeping extraction processes sustainable. Thermal degradation of oligomeric proanthocyanidins (OPCs) is a common hazard in basic spray-drying and extraction loops.
Our technical team employs a low-temperature vacuum concentration process combined with multi-stage membrane filtration to isolate active molecules without subjecting them to prolonged high heat.
Looking forward, our R&D is focused on enzymatic pre-treatments that break down tough botanical cell walls, increasing the yield of bio-active compounds. By introducing targeted food-grade enzymes, we can extract higher volumes of active compounds from raw materials, reducing environmental impact and stabilizing costs for buyers.
Hawthorn extract is a versatile ingredient used across multiple high-growth segments:
We work closely with brand owners to develop customized extracts, matching specific particle sizes, colors, and compound ratios to meet their exact formulation needs.
A Global Leader in Natural Ingredients
Benefiting from the solid foundation provided by its parent company, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. focuses on researching, developing, producing and selling healthy natural ingredients. With more than two decades of industry experience, it has become a leader in the field, specializing in providing high-quality plant extracts and customized solutions to global customers. Services meet the needs of industries including herbal medicine, health foods, dietary supplements, food and beverages, daily chemicals and cosmetics.
Our operations are supported by three companies - Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd. - which together operate 3 production bases covering more than 100 acres and process more than 3,000 tons of plant raw materials each year. The product range includes more than 200 plant extracts, and we also provide a variety of certified organic products to meet the global demand for environmentally friendly and healthy solutions. Exporting to 60% of the world's countries, serving more than 200 countries and regions and more than 500 customers from all walks of life.
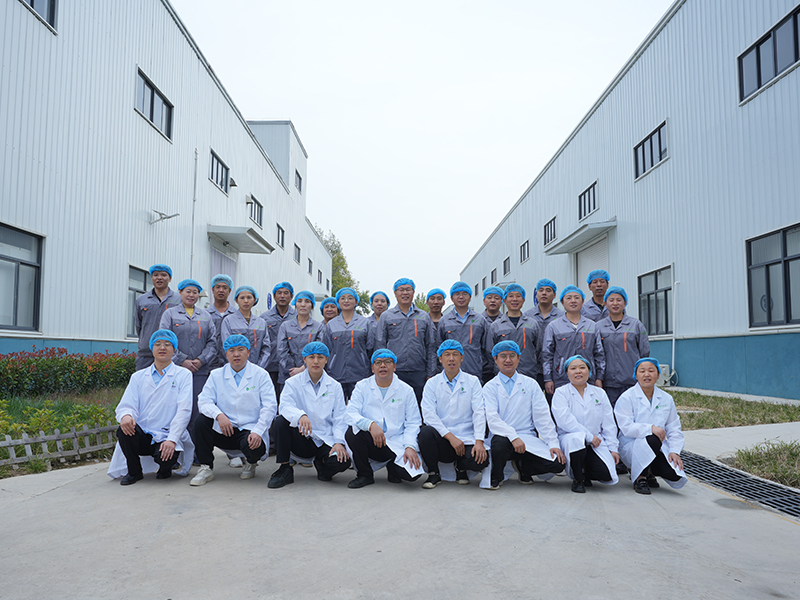
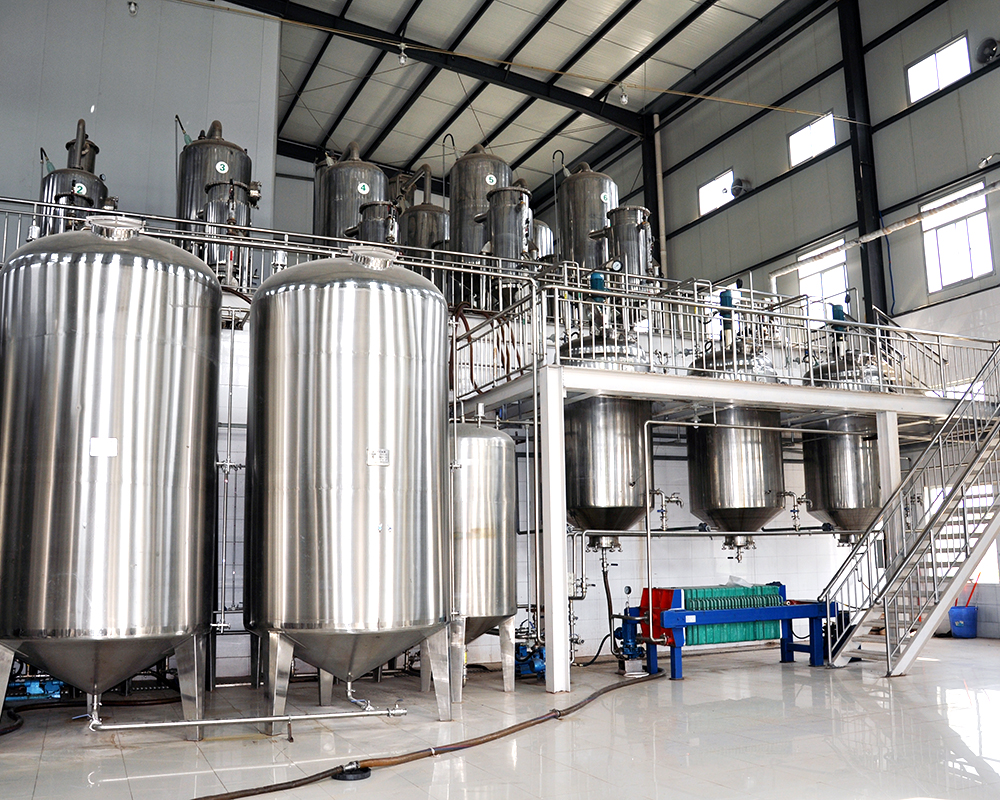
Our first factory was established in 2012 in Sanyuan City, Xi'an, four years after our company was founded. At that time, our production experience was still in its early stages, and we faced many challenges as we worked to refine our processes. However, we remained committed to continuous improvement, investing heavily in technology, training, and quality control to strengthen our capabilities. These early efforts laid a strong foundation for our future growth, shaping the high standards of excellence that we uphold today.
Powder collection, crushing and sieving, mixing and drying processes are all performed in a Class 100,000 cleanroom environment. Our operators strictly follow hygiene protocols and wear sterile gowns, masks and gloves to maintain product purity and safety, thus ensuring that we provide our customers with high quality standards and reliable ingredients.
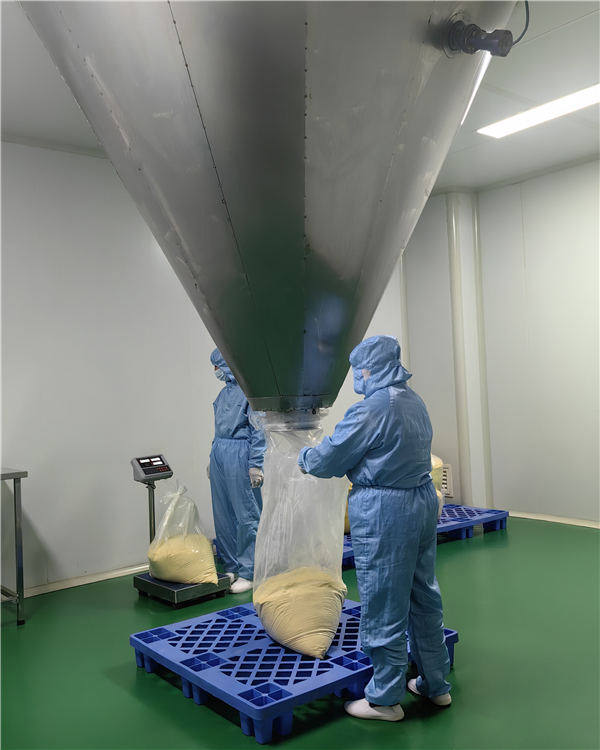
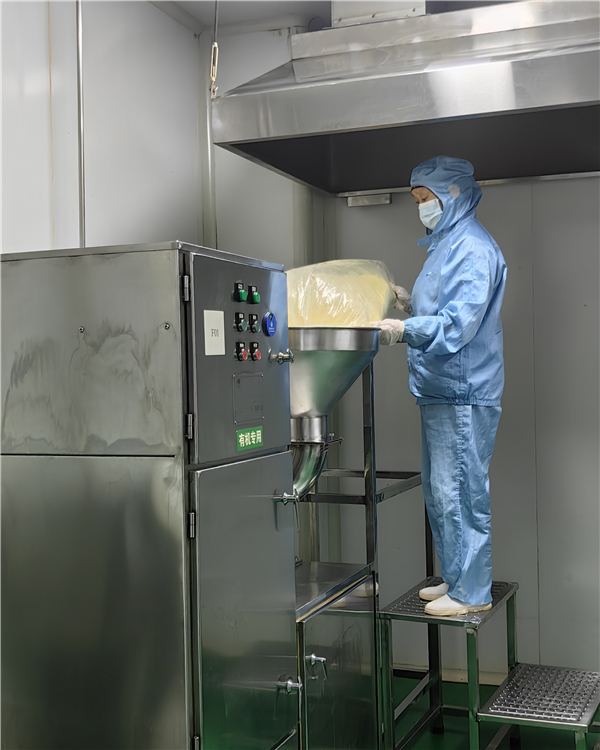
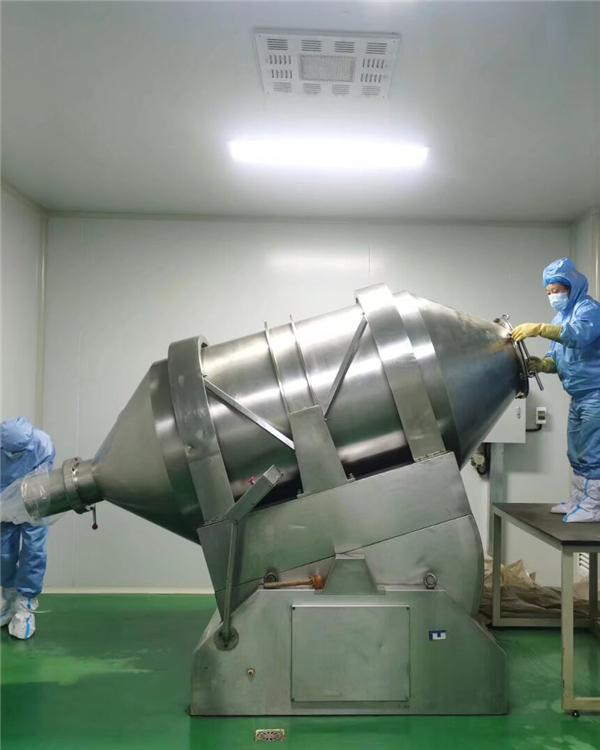
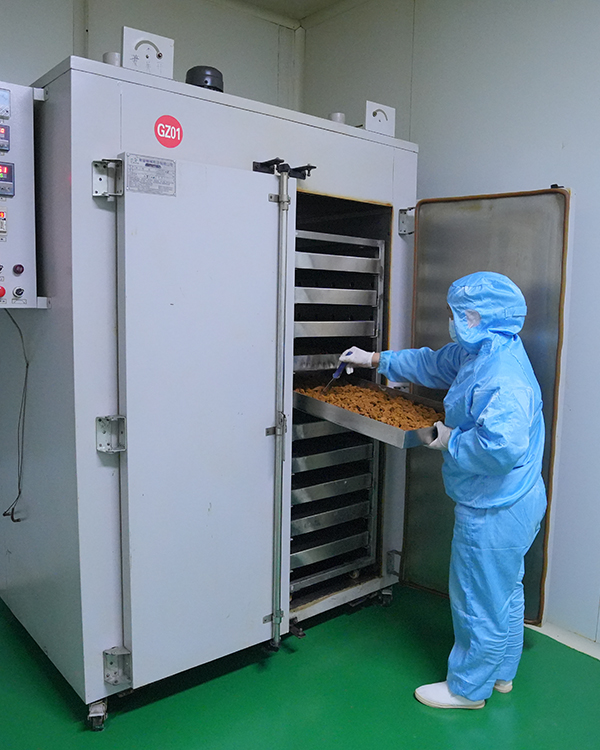
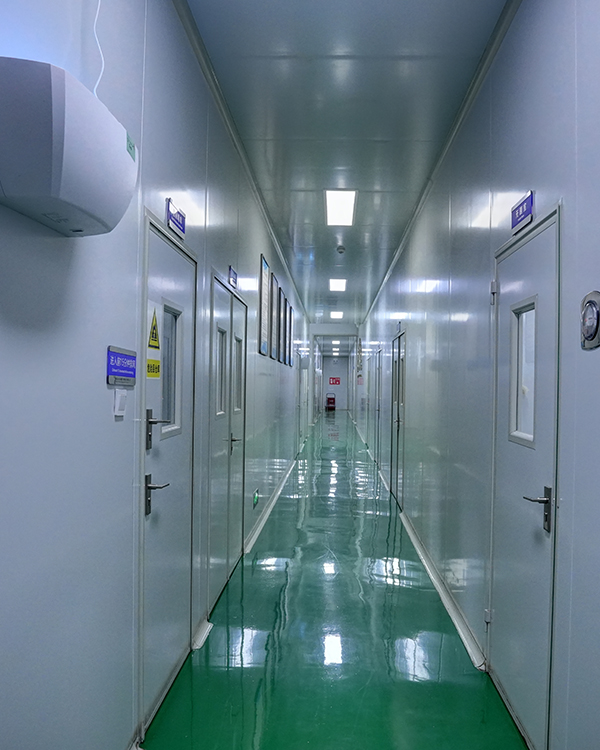
China's Shaanxi province is a key hub for scientific botanical extraction. Operating at the heart of this region, our factories utilize smart manufacturing principles to maintain product consistency. Automation of temperature parameters, solvent ratios, and cycle times removes the risks of human error.
With three production bases spanning over 100 acres, we maintain buffer stocks of raw materials. This helps protect our partners from harvest and market price fluctuations. We work directly with local growers, tracking crops from farm to factory to ensure a stable supply of authentic raw botanicals.
Selling health products globally requires navigating complex local regulations. Botanical Cube Inc. provides extensive documentation to support regulatory approvals. Every shipment comes with a Certificate of Analysis (CoA), Allergen Statement, GMO Declaration, and details on heavy metal, microbiological, and solvent residues.
We assist international buyers with customs registration, import compliance, and local product testing, helping to streamline import procedures.
 Botanical