Engineered for premium nutraceutical, functional food, and cosmetic formulations requiring rigorous standardized potency and certified organic authenticity.
Mapping the growth trajectories, import-export corridors, and supply chain strategies for bioactive organic ingredients in Georgia and North American trade hubs.
Georgia has rapidly expanded its footprint as a strategic nexus for food processing, cosmetic compounding, and pharmaceutical packaging across North America and Eastern European commercial hubs. With major logistical arterial systems connecting deep-water shipping terminals such as the Port of Savannah and regional industrial clusters in Atlanta and Tbilisi, enterprise procurement teams are demanding ultra-transparent, certified organic supply chains. The shift toward clean-label consumer goods has triggered an unprecedented surge in demand for standardized plant extracts, standardized botanical fractions, and certified organic active pharmaceutical ingredients (APIs).
Navigating modern supply chain constraints requires robust partner networks capable of maintaining continuous raw material feeds without compromising regulatory integrity. Global enterprise buyers operating within Georgia require strict adherence to U.S. FDA FSMA (Food Safety Modernization Act), USDA Organic (NOP), European Commission Organic regulations, and local phytosanitary compliance. Key requirements include complete traceability from agricultural cultivation sites to cleanroom packaging facilities, zero pesticide contamination, and rigorous heavy metal testing below international pharmacopeia limits.
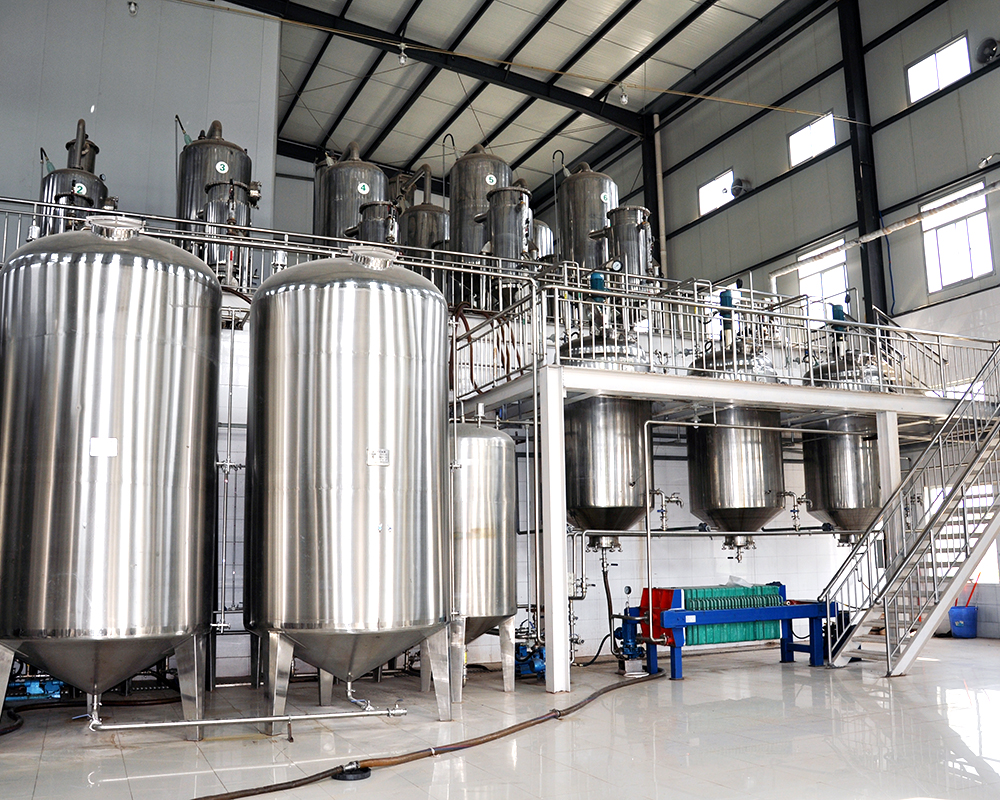
To stand out in competitive markets, functional food, dietary supplement, and personal care manufacturers require advanced processing capabilities. Our manufacturing facilities leverage state-of-the-art spray drying, fluid-bed granulation, and liposomal microencapsulation technologies. These engineered systems preserve fragile molecular structures—such as thermolabile enzymes, cellular antioxidants (e.g., L-Ergothioneine and NADH), and natural pigments (e.g., Phycocyanin)—ensuring optimal stability, extended shelf life, and maximal biological activity upon end-consumer ingestion or topical application.
Full chain-of-custody documentation from organic-certified farms to final cleanroom packaging. Zero synthetic additives, pesticides, or irradiation.
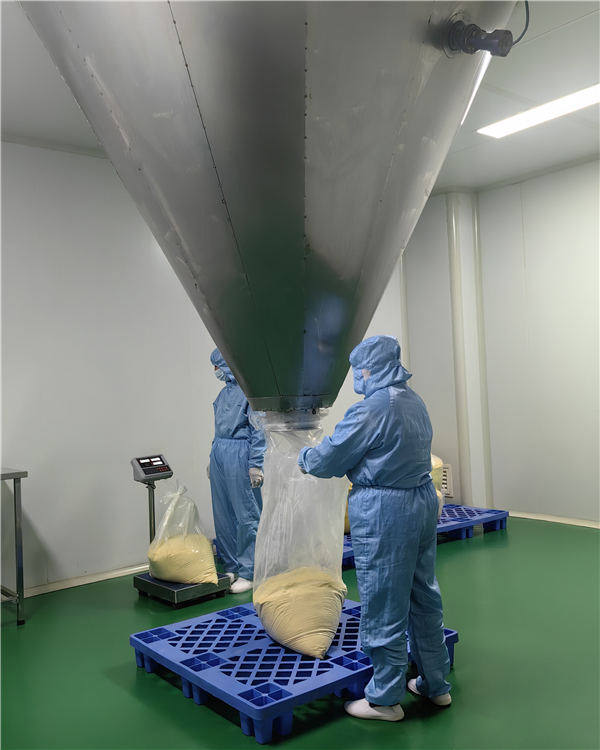
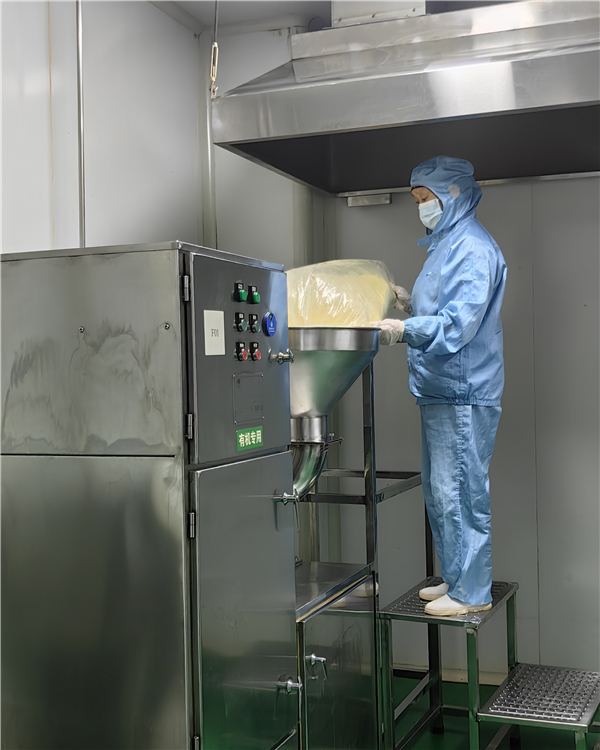
Sieving, blending, micronization, and primary inner packaging performed under strict ISO Class 8 cleanroom environmental conditions.
Flexible contract manufacturing capabilities, including custom mesh sizes (80-200 mesh), customized water solubility ratios, and proprietary blends.
High-demand Active Plant Compounds Formulated for Industrial-Scale Manufacturing.
Leveraging decades of industrial biotechnology excellence to serve food, beverage, nutraceutical, and cosmetic enterprises across 60+ countries.
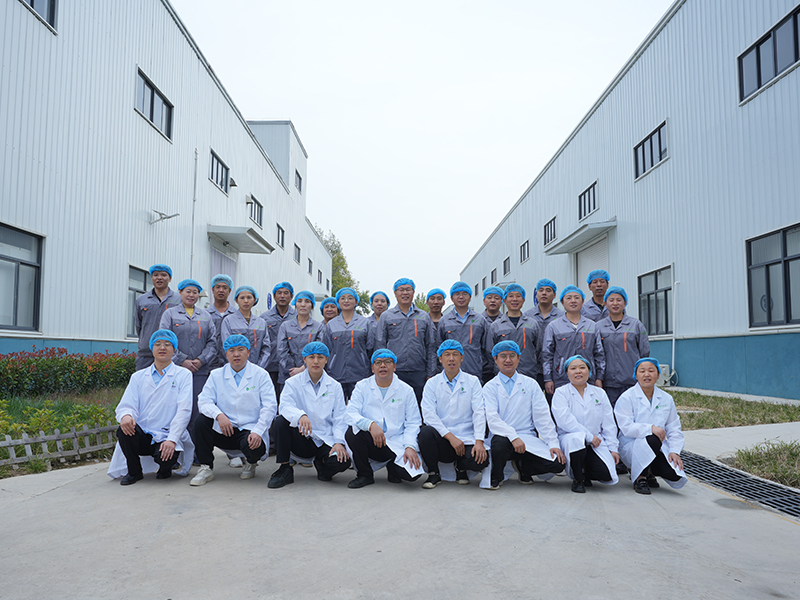
Benefiting from the solid foundation provided by its parent enterprise, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd. operate three state-of-the-art production facilities spanning over 100 acres. With over two decades of industry leadership, our facilities process more than 3,000 metric tons of botanical raw materials annually.
Established in 2012, our flagship Sanyuan Factory serves as the benchmark for cleanroom extraction. Within our 100,000-Class Cleanroom environment, critical processes—including micro-powder collection, ultra-fine crushing, precision sieving, homogenizing, and vacuum low-temperature drying—are performed under strictly monitored atmospheric standards. Operators follow rigorous sterile gowns, mask, and glove protocols to eliminate cross-contamination and guarantee zero microbial compromise.
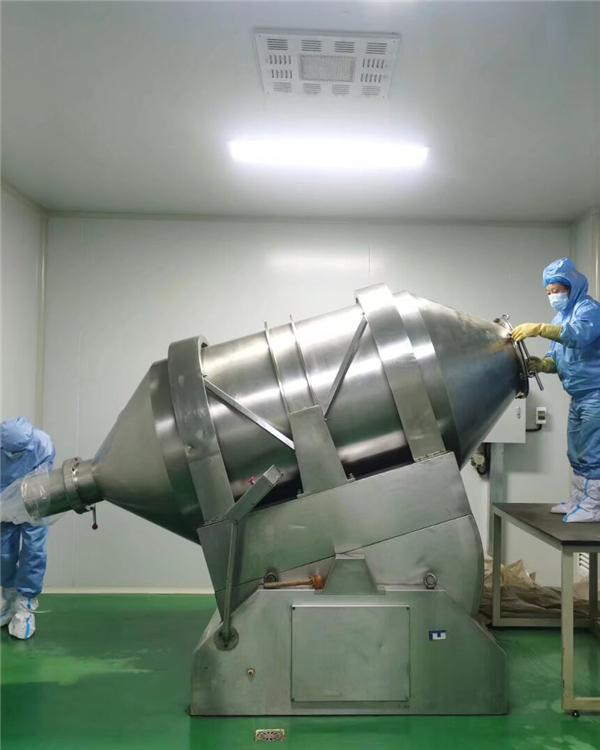
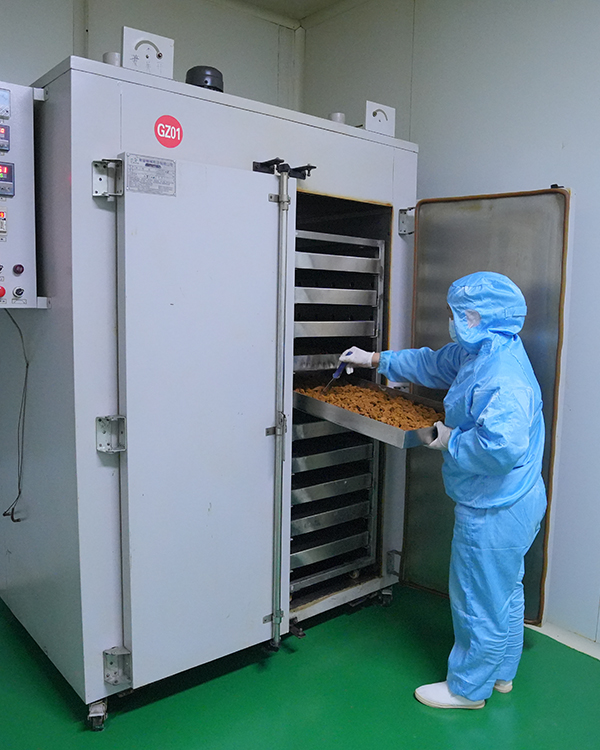
In-depth technical whitepaper detailing our proprietary extraction steps, molecular testing protocols, and compliance guarantees.
To ensure that clients in Georgia receive botanicals of pristine purity and active bio-potency, our technical engineering team implements a closed-loop extraction and refining workflow:
Raw plant materials undergo stringent identity verification using High-Performance Thin-Layer Chromatography (HPTLC) and DNA barcoding. Batches are screened for over 400 pesticide residues, aflatoxins, and heavy metals (Pb, Cd, As, Hg) prior to entering extraction tanks.
Utilizing counter-current ultrasonic-assisted extraction and aqueous or organic food-grade ethanol solvents, active compounds are isolated at optimized low temperatures to preserve molecular ring structures and bio-potency.
Polymeric resin chromatography and ceramic ultrafiltration membranes concentrate key active molecules—such as Matrine, Rosmarinic Acid, or Gingerols—to exact targeted percentages (up to 99% purity).
Concentrated liquids are converted into free-flowing powders via low-temperature spray drying or vacuum freeze-drying within our Class 100,000 cleanroom. Powders are micronized to uniform particle size distributions tailored for tablet compression, capsule filling, or beverage dissolution.
Select from our certified inventory of high-purity functional plant extracts, available in bulk quantities with complete COA and analytical validation.
Detailed insights addressing compliance, shipping logistics, quality testing, and contract manufacturing for enterprise buyers in Georgia.
Elevate your product line in Georgia with standardized, certified organic botanical ingredients backed by 20+ years of industrial extraction expertise. Contact our engineering and sales team today.
Send Inquiry Now Botanical