High-purity botanical raw materials optimized for rapid customs clearance and immediate integration into Algiers pharmaceutical and wellness production lines.
As the largest metropolitan hub in North Africa, Algiers is undergoing a structured transformation within its pharmaceutical and nutraceutical manufacturing ecosystem. Under the guidance of Algeria's Ministry of Pharmaceutical Industry and aligned with state import-substitution mandates, local manufacturers in districts like Rouiba, Oued Smar, and Reghaia are actively pivoting toward domestic formulations featuring premium plant extracts. This systemic transition requires a reliable pipeline of high-concentration phytochemical raw materials capable of satisfying stringent USP (United States Pharmacopeia) and EP (European Pharmacopoeia) monograph standards.
By shifting formulation pipelines from expensive synthetic chemicals to standardized botanical isolates, manufacturers in Algiers are positioning themselves to capture both domestic consumer demand and export pathways into Mediterranean and sub-Saharan African markets. Our supply chain infrastructure offers an answer to this regional transition, guaranteeing physical availability, purity authentication (via HPLC/GC-MS), and zero-barrier custom clearance documents certified to meet Algerian administrative specifications.
For Algiers-based buyers, importing botanical powders requires absolute compliance with local phytosanitary restrictions, non-GMO certifications, and heavy metal limits. The integration of ingredients such as Nobiletin or Corosolic Acid into local formulations demands meticulous documentation. We provide complete dossier support including Certificates of Analysis (COA), Allergen Declarations, and BSE/TSE-Free Certificates to facilitate rapid processing through Algiers Port (Port d'Alger) and Houari Boumediene Airport customs.
A Global Leader in Natural Ingredients
Benefiting from the solid foundation provided by its parent company, Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. focuses on researching, developing, producing and selling healthy natural ingredients. With more than two decades of industry experience, it has become a leader in the field, specializing in providing high-quality plant extracts and customized solutions to global customers. Services meet the needs of industries including herbal medicine, health foods, dietary supplements, food and beverages, daily chemicals and cosmetics.
Our operations are supported by three companies - Xi'an Tianben Bioengineering Co., Ltd., Botanical Cube Inc. and Shaanxi Tianben Kangyuan Biotechnology Co., Ltd. - which together operate 3 production bases covering more than 100 acres and process more than 3,000 tons of plant raw materials each year. The product range includes more than 200 plant extracts, and we also provide a variety of certified organic products to meet the global demand for environmentally friendly and healthy solutions. Exporting to 60% of the world's countries, serving more than 200 countries and regions and more than 500 customers from all walks of life.
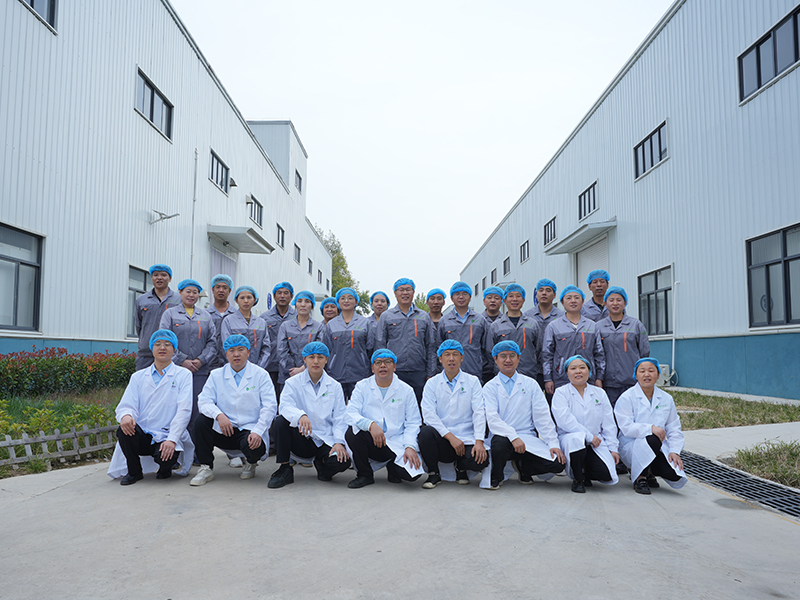
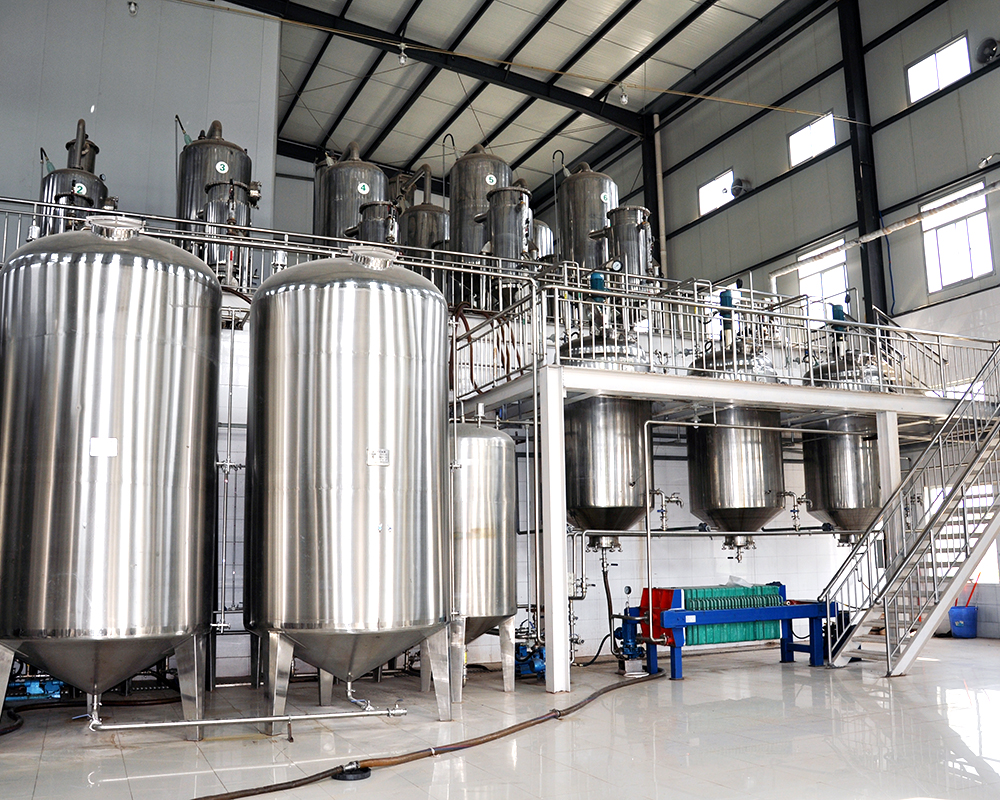
Our first factory was established in 2012 in Sanyuan City, Xi'an, four years after our company was founded. At that time, our production experience was still in its early stages, and we faced many challenges as we worked to refine our processes. However, we remained committed to continuous improvement, investing heavily in technology, training, and quality control to strengthen our capabilities. These early efforts laid a strong foundation for our future growth, shaping the high standards of excellence that we uphold today.
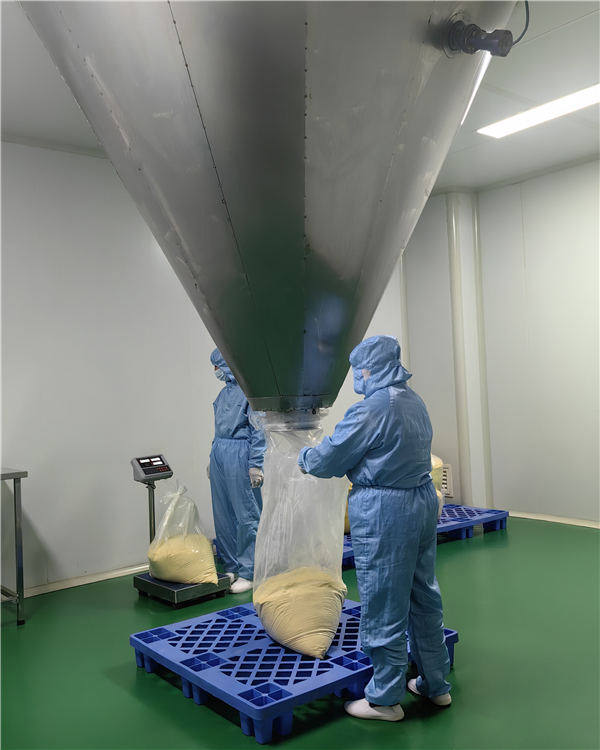
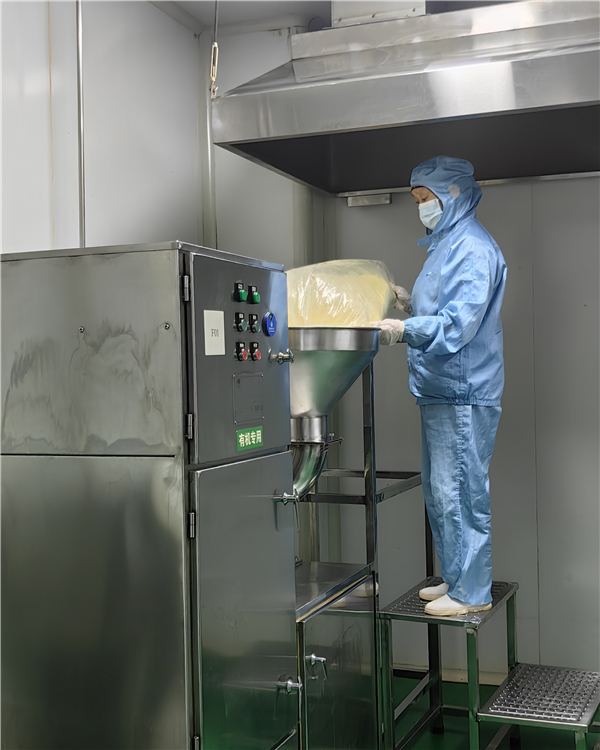
Powder collection, crushing and sieving, mixing and drying processes are all performed in a Class 100,000 cleanroom environment. Our operators strictly follow hygiene protocols and wear sterile gowns, masks and gloves to maintain product purity and safety, thus ensuring that we provide our customers with high quality standards and reliable ingredients.
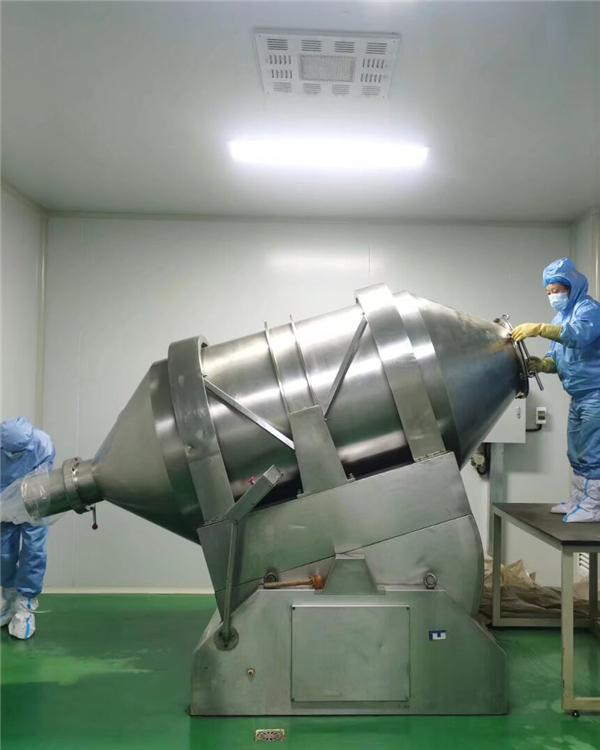
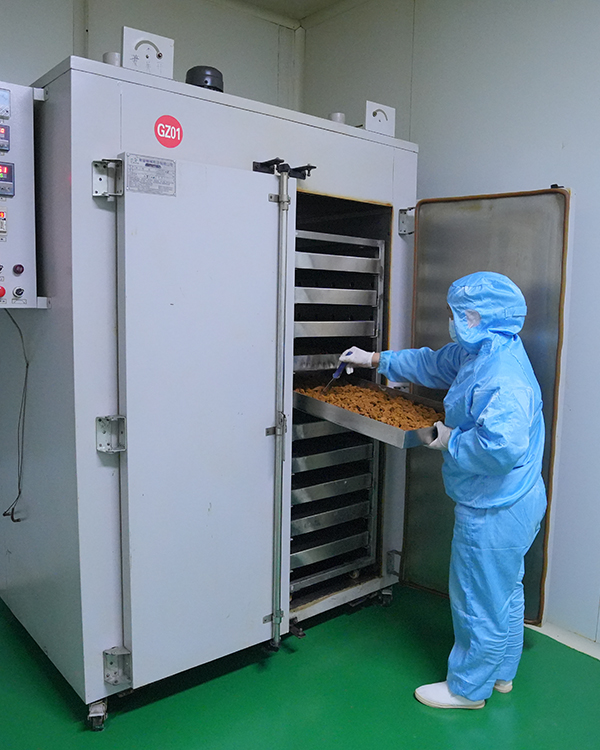
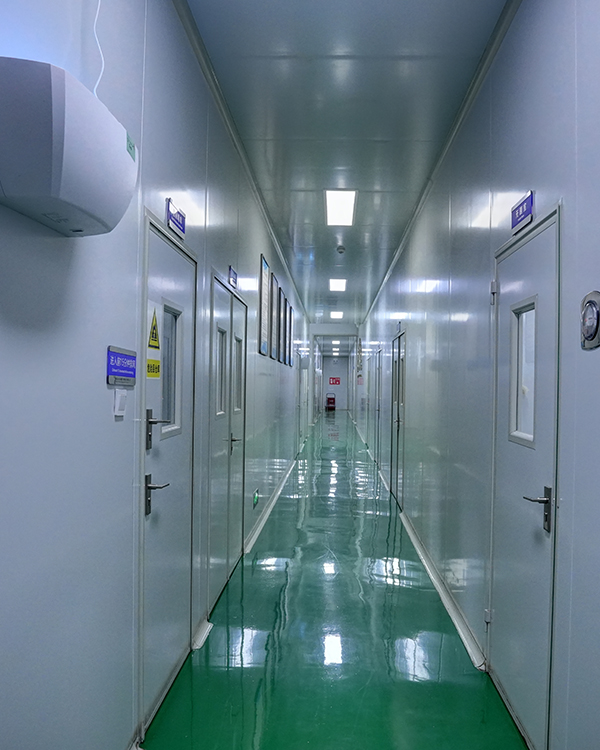
Leveraging Industry 4.0 processes to ensure chemical fingerprint consistency and resilient output cycles for Algiers logistics partners.
Preserving heat-sensitive phytochemical components (such as enzymes and essential volatile oils) through controlled sub-zero extraction protocols, minimizing thermal degradation.
Integrating online HPLC and UV-Vis spectroscopy systems directly into our discharge lines to continuously monitor active compound concentration profiles in real time.
Operating ISO 8 (Class 100,000) air shower purification complexes to guarantee negative microbiological loading for bulk powders intended for Algiers infant formula and drug standards.
For Algiers formulation chemists, the target parameters of natural raw materials represent a strict binary metric. Our products are formulated to integrate seamlessly into diverse production lines:
Understanding the logistical realities of Mediterranean trade lanes, we offer tailored shipping configurations. We provide heavy-duty export drums (25kg net weight) sealed with food-grade double PE liners. Shipments to Algiers are supported by expedited customs clearance paperwork, including Certificate of Origin, Phytosanitary Certificate, and comprehensive HPLC analytical charts.
Select biological agents engineered for therapeutic efficacy and industrial processing stability.
Addressing technical, regulatory, and logistics queries for importing botanical APIs into Algeria.
Secure premium, tested botanical raw materials for your manufacturing operations in Algiers. Access our technical department for custom specifications, compliance dossiers, and free sample runs.
Send Inquiry Now Botanical